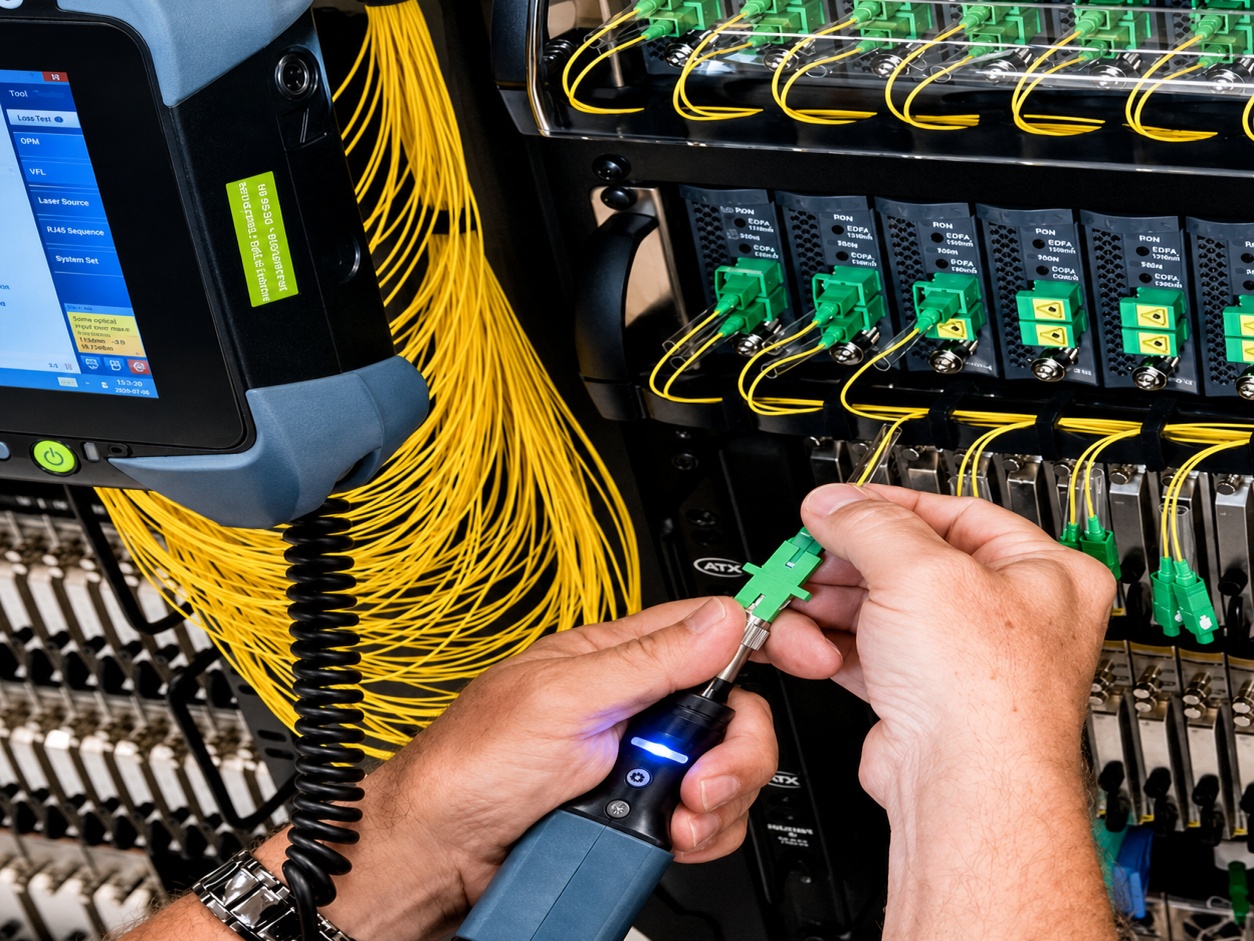
Root-cause analysis in fiber connector systems often begins with the most visible symptom.
Insertion loss increases.
Return loss degrades.
A connector repeatedly needs cleaning.
A patch cord behaves differently after remating.
One port becomes unstable.
A technician replaces the connector and performance returns to normal.
The natural conclusion is that the last visible component caused the problem.
Sometimes that conclusion is correct.
But fiber interfaces are relational systems.
Their behavior emerges from connector geometry, adapter alignment, polish architecture, contamination, mechanical loading, tolerance interaction, mating history, and maintenance conditions.
A visible failure therefore may represent the final stage of a much longer causal sequence.
This is why Fiber Connectors Explained: SC, LC, FC, MPO & VSFF provides essential context. Different connector architectures create different mechanical and operational relationships, so the same optical symptom does not always imply the same physical cause.
The same applies to endface behavior. Fiber Polishing Types: UPC vs APC shows why return-loss problems, incorrect mating, contamination, and endface geometry must be interpreted through the physical architecture of the interface rather than reduced to one generic “bad connector” explanation.
The central engineering law is therefore:
Root causes in fiber connectors and interfaces are often explained backwards because investigations begin with the component or maintenance event that made the problem visible rather than with the sequence of conditions that gradually made the interface vulnerable.
The Last Event Before Failure Is Often a Trigger, Not the Root Cause
A connector interface operates normally.
Maintenance occurs.
The connector is disconnected.
It is cleaned or inspected.
The interface is remated.
Performance becomes abnormal.
The maintenance activity immediately attracts attention.
The sequence appears obvious:
Maintenance happened.
The interface failed.
Therefore maintenance caused the failure.
Sometimes it did.
But the maintenance event may have only exposed a condition that already existed.
The interface may have been operating with limited margin.
Adapter alignment may already have become sensitive.
Contamination may have accumulated.
Patch-cord loading may have increased.
Repeated mating may have changed interface repeatability.
The final maintenance event recreated the physical mating state.
That state happened to reveal the vulnerability.
The deeper question is therefore not only:
What happened immediately before the problem appeared?
It is:
Why did an ordinary maintenance event produce an abnormal result at this particular interface?
That question moves root-cause analysis away from chronology alone and toward the physical conditions that made the trigger consequential.
Engineering Insight
The event immediately preceding a connector failure may explain when the problem became visible, but not necessarily why the interface had become sensitive to that event.
Successful Replacement Can Create False Causal Confidence
Replacement is one of the most common troubleshooting actions.
A connection behaves poorly.
Replace the patch cord.
Performance returns.
The conclusion appears simple:
Bad patch cord.
Operationally, the replacement was successful.
Causally, the explanation may be incomplete.
A replacement changes several variables at once.
Connector geometry.
Endface condition.
Contamination state.
Mating history.
Cable loading.
Tolerance combination with the adapter.
The new interface is physically different from the old one.
Improvement therefore proves that changing the interface restored performance.
It does not always prove that the removed patch cord was independently defective.
This becomes especially obvious when the removed patch cord later performs normally elsewhere.
That result is not contradictory.
It suggests the original problem may have existed in the mating relationship.
Connector A with Adapter X performs poorly.
Connector B with Adapter X performs normally.
Connector A with Adapter Y also performs normally.
No individual component may be outside specification.
The original combination may simply have been less favorable.
Engineering Insight
Replacement success proves that the mating system changed, but it does not uniquely identify which component or relationship created the original instability.
Cleaning Success Can Hide the Mechanism Behind Recurring Contamination
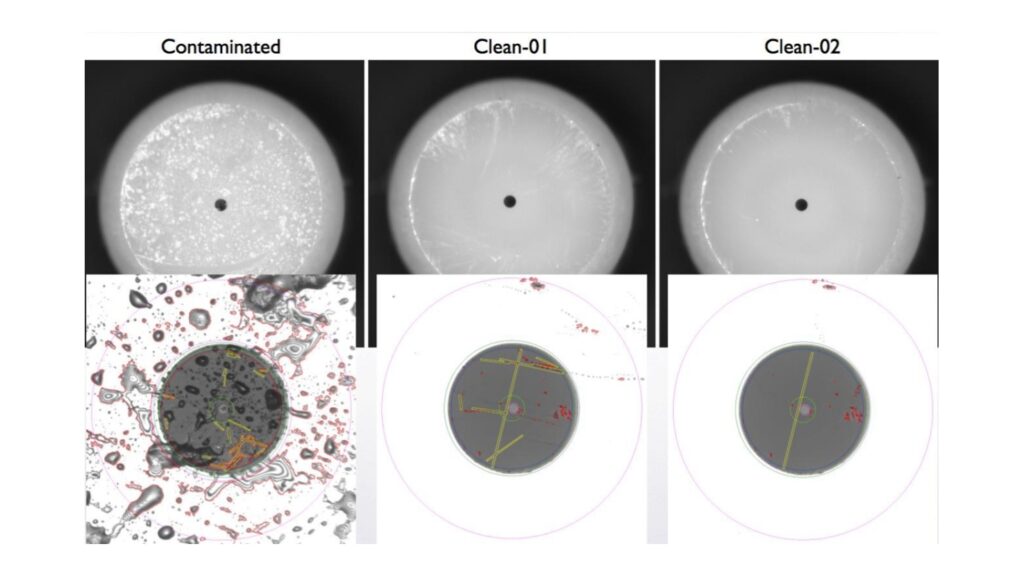
Cleaning creates another common backward explanation.
Loss increases.
The connector is cleaned.
Performance improves.
Therefore contamination was the root cause.
That may be true for the immediate event.
Recurring contamination requires a deeper explanation.
Why does the same interface become contaminated repeatedly?
Why does it require more cleaning than nearby ports?
Why does the problem return after maintenance?
The contamination may be the failure mechanism.
The root cause may lie elsewhere.
Difficult access.
Repeated unnecessary handling.
Poor environmental control.
Contamination transfer from the mating partner.
A contaminated adapter.
Weak capping practices.
High-density maintenance conditions.
If the investigation stops because cleaning restored service, the mechanism that repeatedly recreates contamination remains.
This is one reason corrective success can produce false causal closure.
The symptom disappears.
The system condition survives.
Engineering Insight
Contamination may explain how optical performance degraded, while recurring contamination patterns reveal the deeper operational or environmental condition that keeps recreating the problem.
The Most Visible Connector Often Receives Too Much Blame
Fiber interface failures usually become visible at a connector.
This creates a natural bias.
The connector receives attention because it can be inspected, cleaned, replaced, and measured.
But the interface includes more than the connector.
Adapter sleeve.
Mating partner.
Patch-cord routing.
Mechanical loading.
Endface compatibility.
Contamination environment.
Port accessibility.
A connector may therefore become the visible location of a broader system condition.
For example, a patch cord may repeatedly show unstable performance at one port.
Several patch cords behave normally elsewhere but less consistently at the same location.
The port becomes stronger evidence than any individual patch cord.
Likewise, a connector may appear mechanically normal while external cable strain changes its seating behavior.
The visible component contains the symptom.
The causal mechanism extends beyond it.
This is why component-centered troubleshooting can create repeated misdiagnosis.
The easiest component to replace becomes the easiest component to blame.
Engineering Insight
Visible connector symptoms can overconcentrate causal attention on one component even when the instability is created by the wider mating and mechanical environment.
Adapter Conditions Are Often Discovered Late Because They Are Less Visible
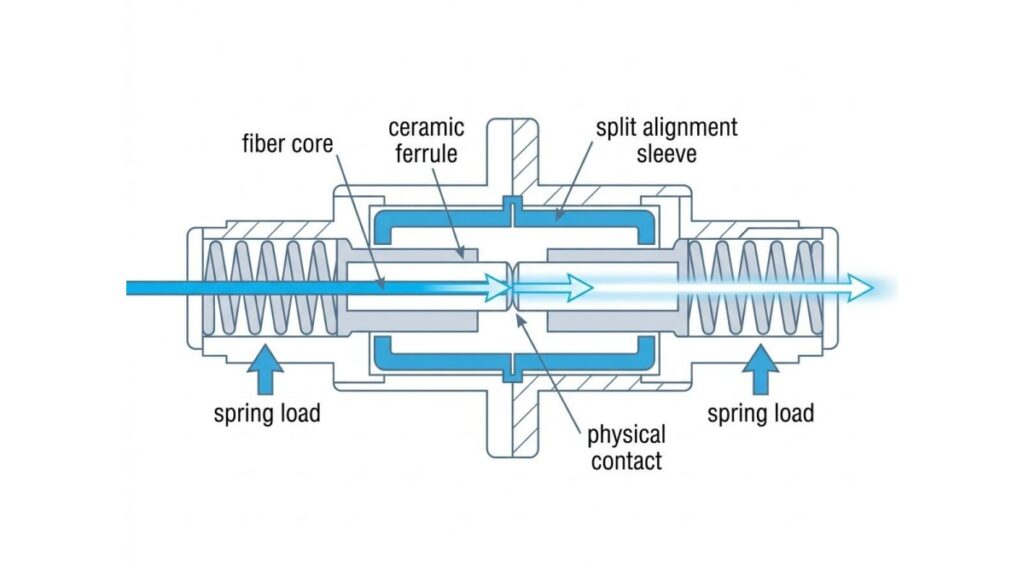
Adapters frequently remain installed while patch cords are changed repeatedly.
This makes them easy to exclude from early troubleshooting.
A patch cord is replaced.
The problem improves.
The adapter remains.
But adapters participate directly in ferrule alignment.
They also accumulate history.
Repeated ferrule insertion.
Contamination.
Sleeve wear.
Mechanical retention changes.
Different connector populations.
A recurring interface problem at one adapter location can therefore originate partly from the common alignment element rather than from successive patch cords.
Because the adapter is less frequently replaced, its role may only become obvious after several connector substitutions fail to produce lasting stability.
The causal story then gets reversed.
Several patch cords are classified as defective.
Only later does the location itself become suspicious.
A stronger root-cause method asks earlier:
Which element is common across repeated failures?
Engineering Insight
Adapter-related mechanisms are often identified late because troubleshooting naturally follows replaceable patch cords first, even though the adapter may be the persistent element across repeated interface problems.
UPC and APC Failures Are Often Explained From the Symptom Instead of the Geometry
Poor return loss appears.
The connector is blamed.
But reflected-power behavior depends on endface geometry.
This is why Fiber Polishing Types: UPC vs APC is essential during causal analysis.
UPC and APC do not manage reflections identically.
APC uses an angled physical-contact geometry.
UPC uses a different physical-contact relationship.
A poor return-loss result can therefore emerge from several mechanisms.
Contamination.
Surface damage.
Incorrect mating.
Geometry deviation.
Poor physical contact.
Polish incompatibility.
The symptom alone does not identify which one.
An APC connector with abnormal reflection behavior should not automatically be classified as “bad APC.”
The stronger analysis asks:
Is the polish type correct?
Is the mating partner compatible?
Is physical contact preserved?
Is contamination present?
Is the endface damaged?
Did the problem appear after remating?
The explanation should proceed from geometry toward measurement.
Not from measurement directly toward component blame.
Engineering Insight
Return-loss symptoms should be traced through actual polish geometry and mating condition because the same optical result can emerge from different physical mechanisms.
Mechanical Loading Is Often Mistaken for an Optical Component Problem
Connector failures appear optically.
The underlying cause can be mechanical.
A dense patch field applies lateral load.
A patch cord is routed too tightly.
A bundle is moved.
A connector housing experiences strain.
Performance changes.
The first response may focus on endface contamination or connector quality.
The actual problem may exist behind the connector.
This happens because the measurement occurs at the optical interface while the causal force originates elsewhere.
Mechanical loading is therefore easy to underweight.
The interface may appear normal during inspection.
When the patch cord is relaxed, performance improves.
When neighboring cables are moved, the condition changes again.
These observations reveal a broader mechanical system.
Ferrule contact.
Housing engagement.
Adapter retention.
Patch-cord strain.
Bundle interaction.
High-density systems make this more common because individual patch cords have less mechanical independence.
Engineering Insight
Optical symptoms can be produced by mechanical conditions outside the ferrule interface, so connector troubleshooting must include the routing and loading environment surrounding the connection.
Repeated Remating Can Make the Wrong Explanation Look Right
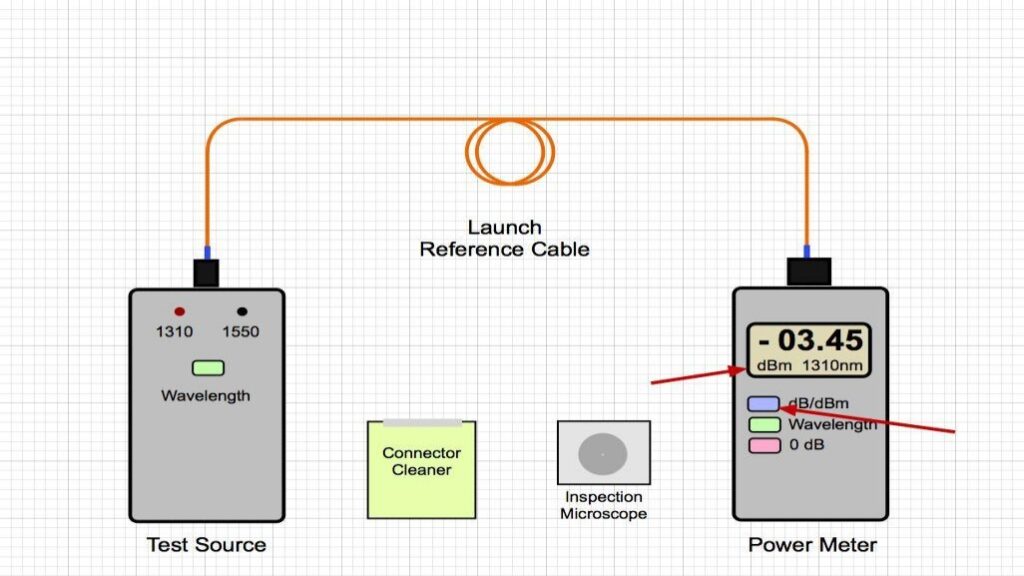
Suppose a connector shows elevated loss.
It is remated.
The result improves.
The technician concludes that the original mating was poor.
That explanation is plausible.
But repeated remating changes multiple conditions.
Ferrule seating.
Adapter relationship.
Particle position.
Contact force.
Cable loading.
The next state may simply be more favorable.
If performance varies substantially across repeated controlled mating cycles, the real lesson is not that one mating was wrong.
It is that the interface is sensitive to mating state.
That sensitivity itself may originate from:
Tolerance stacking.
Adapter condition.
Contamination.
Endface geometry.
Mechanical load.
The remating event therefore should not always be treated as the cause.
It can be a diagnostic probe.
Engineering Insight
When remating changes performance repeatedly, the important causal evidence is interface sensitivity rather than the assumption that one previous mating event was simply incorrect.
Multi-Fiber Systems Reveal Why Failure Patterns Matter More Than Single Symptoms
Multi-fiber interfaces complicate backward causal reasoning further.
One physical mating event supports several channels.
Suppose one channel shows elevated loss.
The immediate instinct may be to blame one fiber position.
That may be correct.
If several adjacent channels show similar degradation, a shared mechanism becomes more likely.
Contamination pattern.
Ferrule geometry.
Mating pressure.
Alignment condition.
If all channels shift after remating, the interface-level relationship deserves even more attention.
This is why the connector architectures described in Fiber Connectors Explained: SC, LC, FC, MPO & VSFF require different causal models.
A single-fiber failure can often be analyzed one path at a time.
A multi-fiber failure contains spatial information.
The pattern across channels reveals whether the cause is local or shared.
Ignoring that pattern can lead to overly simple component explanations.
Engineering Insight
Multi-fiber failure patterns provide causal evidence because correlated channel behavior can distinguish local fiber problems from shared interface mechanisms.
Recurring Failures at One Location Usually Point Beyond Random Component Defects
One failed connector can be random.
Two failures may still be coincidence.
Repeated failures at the same physical location create stronger evidence.
Different patch cords.
Same port.
Different technicians.
Same instability.
Different times.
Same cleaning requirement.
At this point, repeated individual component defects become a weaker explanation.
The common location becomes more important.
Adapter condition.
Panel access.
Mechanical loading.
Contamination environment.
High local mating frequency.
Poor identification.
Recurring intervention.
Root-cause analysis should therefore look for persistence.
What stays the same across repeated events?
The connector may change.
The adapter remains.
The location remains.
The cable-management environment remains.
The maintenance pattern remains.
The persistent element often provides stronger causal direction than the failed component.
Engineering Insight
Recurring interface problems should be analyzed around the elements that remain constant across events rather than repeatedly attributing each failure to the replaceable component that happened to be present.
Failure Thresholds Encourage Investigations to Start Too Late
Many root-cause investigations begin only after a specification limit is crossed.
Insertion loss becomes unacceptable.
Return loss fails.
Service becomes unstable.
Before that moment, smaller signals may have existed.
Gradual loss increase.
More cleaning.
Greater remating variability.
More technician attention.
Increasing mechanical sensitivity.
Because the interface still passed, these signals were not treated as failures.
Once the threshold is crossed, investigators naturally focus on the final change.
This reverses the causal story.
The final event may only represent the last step in a longer progression.
A stronger investigation therefore includes pre-failure history.
How did the interface behave six months earlier?
Was maintenance frequency increasing?
Did performance become more variable?
Did patch-cord routing change?
Was the port population becoming denser?
The root cause may become visible only when the timeline is expanded.
Engineering Insight
Threshold-based failure detection can make the final event appear causal because earlier signals of declining interface margin were not treated as part of the same failure process.
Hindsight Bias Makes Causal Stories Look Simpler Than They Were
After a failure, the outcome is known.
This changes how earlier events are interpreted.
A maintenance activity now looks suspicious.
A previous cleaning event seems important.
A slightly elevated measurement appears predictive.
A patch-cord routing change suddenly seems obvious.
The investigation can construct a clean story backward from the known outcome.
Real systems rarely evolve that neatly.
Several conditions may have developed simultaneously.
Contamination increased.
Density rose.
Adapter history accumulated.
Patch-cord loading changed.
The interface remained stable because enough margin remained.
One final event made the combined condition visible.
A stronger method reconstructs the interface chronologically.
Original condition.
Changes in component population.
Maintenance events.
Remating history.
Measurement trend.
Routing changes.
First abnormal signals.
Final trigger.
This timeline helps separate cause from hindsight.
Engineering Insight
Chronological reconstruction reduces hindsight bias by showing how interface margin changed before the final failure became visible.
Root Causes Often Form Chains Rather Than Single Events
Complex interface failures often contain several causal layers.
For example:
Density increases.
Patch-cord routing becomes tighter.
Mechanical load on one port increases.
Mating repeatability declines.
The interface begins showing variable insertion loss.
The connector is cleaned repeatedly.
One later remating produces unacceptable loss.
Which event is the root cause?
The remating?
The mechanical loading?
The increased density?
The cable-management design?
The answer depends on how deeply the analysis needs to go.
A useful framework is:
Visible symptom → trigger → failure mechanism → enabling condition → system assumption
The symptom may be high insertion loss.
The trigger may be remating.
The mechanism may be unfavorable alignment.
The enabling condition may be external mechanical loading plus limited tolerance margin.
The system assumption may be that existing patch-cord density would not significantly affect connector mechanics.
Each layer provides different corrective value.
Replacing the connector addresses the symptom.
Improving cable management addresses the enabling condition.
Reconsidering density and routing assumptions prevents recurrence elsewhere.
Engineering Insight
Root causes in connector systems often exist as causal chains, and deeper layers usually provide more transferable engineering lessons than the immediate trigger.
Better Root-Cause Analysis Starts With Relationships, Not Components
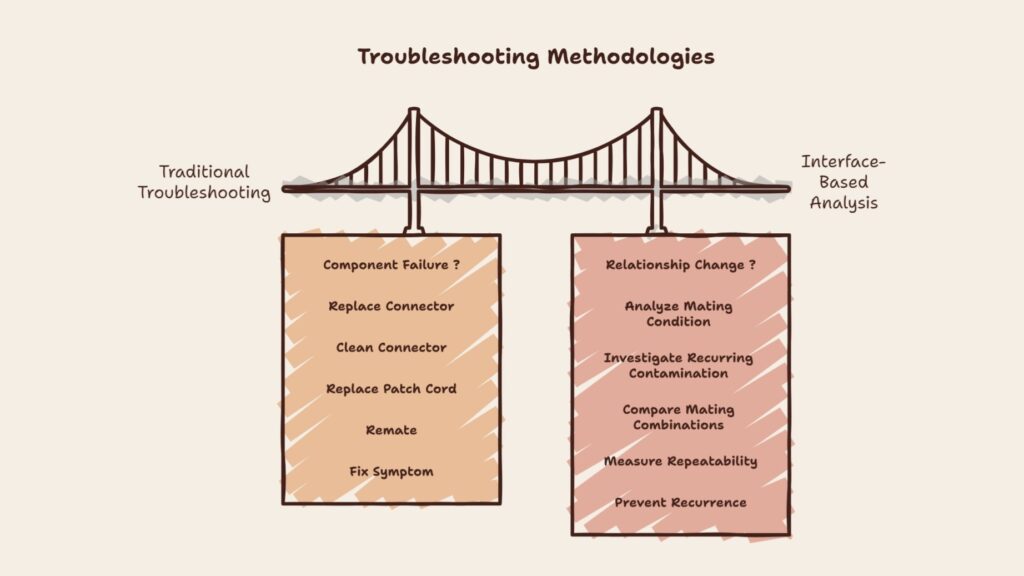
Traditional troubleshooting often asks:
Which component failed?
A stronger interface-based investigation asks:
Which relationship changed?
Connector to connector.
Connector to adapter.
Ferrule to sleeve.
Endface to endface.
Patch cord to connector housing.
Polish geometry to mating partner.
Technician process to contamination state.
Maintenance activity to interface history.
This changes the investigation boundary.
The objective is not avoiding component replacement.
Replacement remains a powerful diagnostic and restoration tool.
The objective is preventing replacement from becoming the entire explanation.
A component can participate in a failure without independently creating it.
A relationship can fail even when every component is acceptable individually.
This is the core difference between component diagnosis and interface diagnosis.
Engineering Insight
Interface root-cause analysis becomes stronger when the primary question shifts from identifying a bad component to identifying the relationship that became unstable.
Root-Cause Analysis Should Change Future Interface Engineering
A root cause is valuable only if it changes future decisions.
If the conclusion is:
Dirty connector.
The response may be:
Clean better.
If deeper analysis shows contamination repeatedly develops because access is poor, the design lesson changes.
Improve maintainability.
If the conclusion is:
Bad patch cord.
The response may be:
Replace patch cord.
If analysis shows tolerance-sensitive behavior repeatedly occurs with one adapter population, qualification or troubleshooting practices may need to change.
If the conclusion is:
Poor remating.
The response may be:
Train technicians.
If mechanical loading from dense patching is the enabling condition, cable management also needs redesign.
Deeper causes create more transferable corrections.
This creates a learning loop:
Field symptom.
Interface analysis.
Causal chain.
System correction.
Updated practice.
Better future infrastructure.
Without that loop, organizations repeatedly restore interfaces without improving the system that keeps producing the same conditions.
Engineering Insight
The strongest root-cause explanation is the one that changes the system condition capable of producing similar interface failures again.
Conclusion
Root causes in fiber connectors and interfaces are often explained backwards because troubleshooting begins where the problem becomes visible.
The patch cord that was replaced.
The connector that was dirty.
The adapter port showing elevated loss.
The maintenance event immediately preceding failure.
The remating that restored performance.
These observations matter.
They often identify triggers or failure mechanisms.
They do not always identify the condition that made the failure possible.
Connector interfaces are relational systems.
Tolerance combinations matter.
Adapters matter.
UPC and APC geometry matters.
Contamination can recur because the environment remains uncontrolled.
Mechanical loading can create optical symptoms.
Multi-fiber channel patterns can reveal shared mechanisms.
Repeated failures at one location can outweigh individual component diagnoses.
Successful replacement can restore service without uniquely identifying root cause.
The stronger causal sequence therefore runs forward:
System assumptions → evolving operating conditions → reduced interface margin → enabling mechanism → trigger → visible optical symptom.
Root-cause investigations usually encounter that sequence in reverse.
The engineering challenge is to reconstruct it correctly.
That means asking more than:
Which connector was present when the failure occurred?
It means asking:
What changed in the complete mating system, which condition had been developing beforehand, and why did this particular interface become unable to absorb an event that similar interfaces could tolerate?
That is where root-cause analysis becomes useful beyond troubleshooting.
It stops explaining only why one connection failed.
It begins explaining what the system must change so that the same causal chain does not quietly rebuild itself somewhere else.
 Get Your Best Price Now!